3-in-1 Filling Machine Manufacturer: Streamlining Your Production Line
2026-10-18
Maybe you know the frustration: three separate machines, three sets of changeovers, and a line that stalls whenever one step falls behind. Wanying Machinery built its 3-in-1 filling machine to collapse washing, filling, and capping into a single, smooth process. In this post, we'll explore what that consolidation really means for your output, your floor space, and your daily workflow.
One Machine, Three Essential Jobs
Most workshop tools force you to choose between floor space and capability. This one doesn't. It takes three tasks that used to need separate stations—truing an edge, flattening a face, and bringing stock to final thickness—and puts them into a single cast-iron frame. You move from one operation to the next without re-clamping or hauling boards across the room.
The first job happens on the infeed table, where a helical cutterhead levels the face of rough lumber. A quick flip of the fence lets that same cutterhead straighten an adjacent edge. Then, instead of switching machines, you raise the bed and feed the board through the thicknessing side; the reference surface you just created guides the cut. Because the three operations share one motor and one reference system, results stay consistent from board to board.
What really stands out is how much time comes back. No more triple-checking settings on three different tools, no more fighting a warped board through a machine that wasn't meant to handle it. You set it once, run the stock through in sequence, and move on to joinery or assembly. It's the kind of quiet efficiency that only shows up when a machine is designed around the work, not the other way around.
Where Rinsing, Filling, and Capping Meet
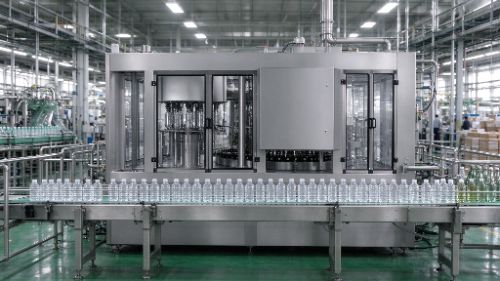
The point where rinsing, filling, and capping converge is often the most rhythm-sensitive zone on a packaging line. Each action depends on the previous one finishing cleanly, yet none can afford to wait. A bottle that leaves the rinse station carrying even a few stray droplets can compromise fill accuracy or, worse, trigger a capping fault downstream. This intersection forces equipment designers to think in milliseconds and millimeters, aligning star wheels, transfer screws, and servo-driven nozzles so that containers move through the sequence without hesitation.
What makes this handoff so unforgiving is that each step has its own tolerance stack. Rinsing demands full inversion or high-pressure ionized air, which can unsettle lightweight containers if the timing drifts. Filling then needs a stable neck reference, yet the bottle is still settling from the rinse turret. Capping, in turn, must grip a closure and apply torque only when the fill level has stabilized. A well-tuned line handles these micro-interruptions invisibly, using buffering zones that absorb tiny speed variations so the three functions never collide.
Operators who understand this intersection learn to watch for subtle signs: a faint rattle at the rinse-to-fill transfer, a recurring capping angle shift on one lane, or foam patterns that suggest a fill nozzle is compensating for excess moisture. Rather than adjusting a single machine in isolation, they trace the symptom back to the shared boundary. When rinsing, filling, and capping meet without friction, the line’s overall efficiency becomes greater than the sum of its individual stations.
Why Fewer Transfers Mean Fewer Defects
Every time a piece of work changes hands, something gets lost. A developer hands off code to a tester, a machinist passes a part to the next station, a designer sends specs to an engineer. Each transfer introduces a moment where assumptions diverge, details blur, or context evaporates. Fewer transfers mean fewer opportunities for that quiet erosion of understanding—and fewer chances for a defect to slip through the cracks.
Think of a game of telephone. You start with a clear message, but by the fourth or fifth whisper, the words have shifted. Manufacturing and software projects work the same way. A tolerance that was obvious to the first person becomes a guess for the third. A requirement that seemed straightforward in a meeting turns vague in an email thread. Cutting down the number of handoffs keeps the original intent closer to the surface, so the final output matches what was actually needed.
There's also a practical side. Each transfer usually brings its own paperwork, validation, or rework loop. Those extra steps don't just slow things down—they create pressure to rush, and rushing breeds mistakes. When you reduce transfers, you reduce the places where people take shortcuts, overlook a specification, or assume someone else already checked. Defects don't appear out of nowhere; they accumulate at the edges of every handoff.
A Smaller Line That Still Hits Your Output Targets
Most compact systems sacrifice speed for square footage. This line was built the other way around. The team started with the required units per hour, then worked backward through every stage—feeding, forming, packing—to cut wasted motion and floor space without touching cycle time. The result is a footprint roughly a third smaller than the previous setup, while the daily count stays exactly where it was.
What makes that possible isn't a single big change. Small adjustments add up: narrower conveyors that move product just as fast, tooling mounted on shared frames, and controls consolidated into one cabinet instead of three. Operators still reach everything without extra walking, and changeovers take no longer than before. If your output target is fixed and your floor isn't, this is the line that says you don't have to choose.
Questions to Ask Before You Choose a Manufacturer
Digging into a manufacturer's track record can reveal more than any polished sales pitch. Ask for specific examples of clients they've worked with in your niche, not just a generic list. If they hesitate to share references or only offer vague case studies, that's a red flag. You want a partner who can point to measurable outcomes—like reduced defect rates or faster turnaround times—without making you chase down the details.
Production capacity and scalability are often overlooked until it's too late. Don't just ask if they can handle your current order volume; press them on how they manage sudden spikes or seasonal demand. A manufacturer that relies on a single production line or a handful of key workers may crumble when you need to double output. Request a walkthrough of their scheduling process and ask what happens when a machine breaks down mid-run. The answers will tell you whether they're truly prepared or just hoping for the best.
Quality control isn't a one-time checkpoint—it's a system. Ask how they document inspections, where they catch defects, and what happens to rejected batches. If their answer is "we check everything at the end," that's not good enough. You need to know if they perform in-process checks, whether they use statistical sampling, and how quickly they can trace a problem back to its source. A manufacturer that can't explain their QC flow in plain language probably doesn't have one worth trusting.
Inside the Changeover That Takes Minutes, Not Hours
The first thing you notice is how the old bottleneck just disappears. A line that once went quiet for half a shift now hums back to life before the coffee in someone’s mug has cooled. The difference isn’t a new machine or a bigger budget—it’s the way every step of the swap has been stripped of waiting. Tools hang where hands naturally reach, not where they were last dropped. Each die or fixture sits on a pre-rolled cart with its own torque spec taped to the handle. Nobody has to hunt for a bolt, guess at a setting, or wander off to borrow a wrench.
There’s a rhythm to it now, almost like a pit crew working on a race car. One operator loosens while another aligns, and a third is already running the first test piece. The veteran who used to roll his eyes at the word “kaizen” just shrugs and says the old way was mostly waiting dressed up as work. Changeover used to mean a long break for maintenance and a slow restart for everyone else. Now it’s a few focused minutes, a quick checklist, and the line is back to making parts instead of burning daylight.
FAQ
It combines rinsing, filling, and capping into a single automated line, so containers move through all three stages without intermediate transfers or manual handling.
Beverages, dairy items, pharmaceuticals, cosmetics, and household chemicals all run smoothly because the machine handles a broad range of liquid viscosities and container shapes.
By merging three separate steps into one continuous process, you cut down on conveyor transfers, eliminate waiting time between stations, and lower the chance of contamination from open containers.
Yes, most models include adjustable guide rails and tool-free change parts. Operators can switch from small vials to larger bottles in a few minutes, and the capping head can be swapped for screw, snap, or sports caps.
Look at their experience with your production volume, the availability of local spare parts, and whether they provide custom options like servo-driven filling or cleanroom compatibility. A video of the machine running your actual product is also a good sign.
A daily washdown of contact surfaces and weekly lubrication of moving parts are usually enough. Machines with stainless steel frames and sealed bearings require less frequent service, and a preventive check every 500 operating hours is recommended.
Often yes. A manufacturer can integrate a new monoblock filling-capping unit with your current conveyor and labeling equipment, as long as speeds and pitch are compatible. A site survey helps determine the best retrofit approach.
Conclusion
The 3-in-1 filling machine fundamentally rethinks how production lines handle rinsing, filling, and capping by consolidating them into a single, compact unit. Instead of moving containers through separate stations—each introducing transfer points, alignment errors, and potential contamination—this integrated approach keeps every bottle or jar under one roof from start to finish. That means fewer conveyor handoffs, less chance for defects like misaligned caps or dripping product, and a significantly smaller footprint without sacrificing throughput. In practice, manufacturers who switch to a 3-in-1 system often report hitting the same output targets they previously achieved with three standalone machines, but with lower maintenance overhead and a cleaner, more predictable workflow.
The real difference, however, shows up during changeovers. A well-designed 3-in-1 unit can switch between bottle sizes and fill volumes in minutes, not hours, because the rinsing, filling, and capping heads are calibrated as one synchronized system rather than three separate islands that need individual adjustment. Before choosing a manufacturer, you need to ask hard questions about changeover time, part accessibility, and whether the machine truly integrates all three functions or merely stacks them on a shared frame. The best suppliers won't just sell you hardware—they'll help you map out how removing transfer points and shortening setup times directly reduces defect rates and labor costs. That's where streamlining stops being a buzzword and becomes a measurable advantage on your floor.
Contact Us
Contact Person: Tyson
Email: [email protected]
Tel/WhatsApp: +8613396971296
Website: https://www.wanyingmachinery.com