High Temperature Defoamer Manufacturer: Key Factors for Reliable Industrial Foam Control
2026-10-10
High-temperature foam control is a make-or-break challenge for industrial operations. A defoamer that fails under heat doesn't just waste money—it stalls entire production lines. That's why selecting a manufacturer with proven thermal expertise is non-negotiable. EVO, a trusted name in industrial foam control, tackles these extremes head-on. But what exactly makes a high-temperature defoamer reliable? Here are the key factors you need to weigh before making your next move.
Understanding Foam Behavior in High-Heat Systems
When temperatures climb, foam doesn't simply disappear—it transforms. In high-heat systems, the liquid films between bubbles thin rapidly as viscosity drops and evaporation accelerates. Surfactants that stabilized foam at room temperature can lose their grip, leading to either sudden collapse or, paradoxically, a stubborn dry foam that resists drainage because the remaining liquid is too scarce to flow. Observing this shift reveals why many industrial defoamers fail exactly when heat is most intense.
Thermal expansion also forces gases trapped in foam to swell, stretching bubble walls beyond their elastic limit. This creates a cascade: larger bubbles merge with smaller ones, and the foam structure coarsens unevenly. In closed vessels, the pressure from expanding foam can trigger unexpected releases, while in open systems, the top layer may bake into a crust that insulates the wet foam below. Engineers who track these dynamics learn to adjust chemical dosing by temperature, not just by volume.
Material choice matters more at high heat. Silicone-based antifoams, for example, often spread better on hot surfaces because lower surface tension lets them penetrate the bubble walls faster. Yet too much heat can volatilize carrier oils, leaving behind a residue that actually stabilizes new foam. The key is timing—introducing the antifoam when the system reaches a critical viscosity range rather than waiting for full thermal equilibrium. Small batch tests that mimic the heat curve of production runs uncover these turning points far better than static jar tests at room temperature.
Selecting Chemistries That Withstand Thermal Stress
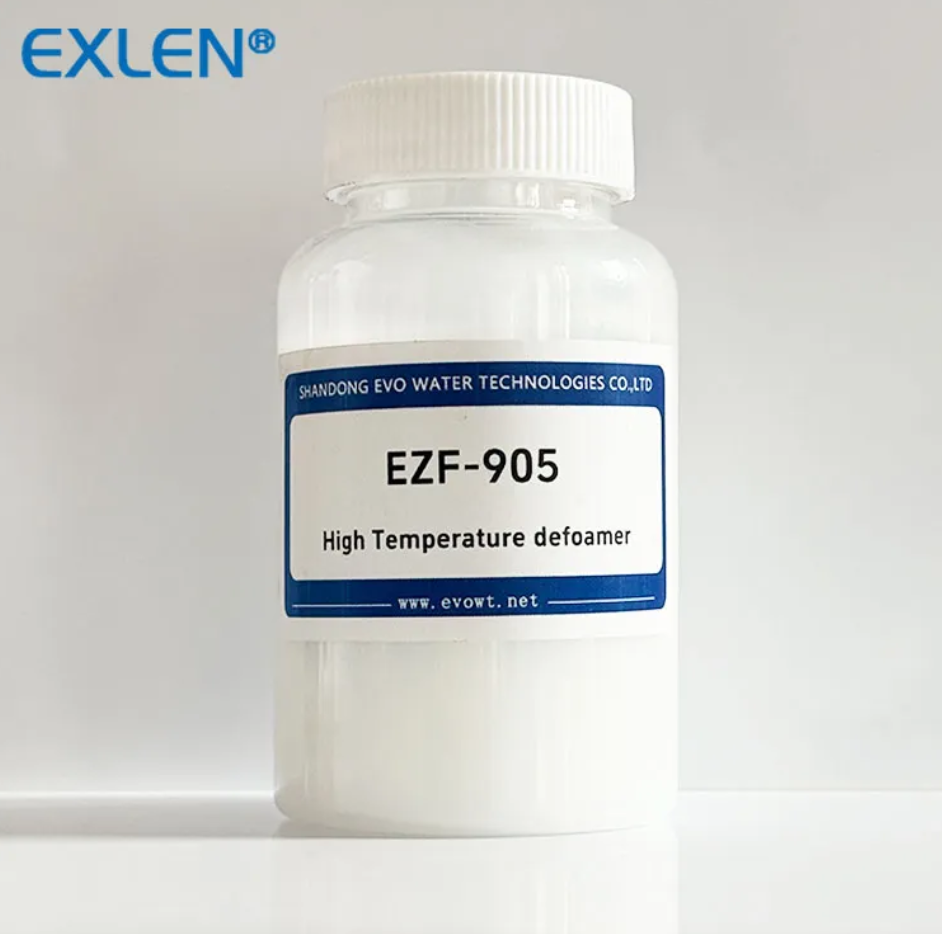
Thermal stress rarely announces itself as a single dramatic event. It builds through repeated expansion and contraction, through long soaks near a material's upper service limit, and through the slow, cumulative damage of oxidation. A chemistry that performs flawlessly at room temperature can crack, delaminate, or lose adhesion when the temperature swings by a hundred degrees every few hours. The first practical filter is therefore not the datasheet's maximum temperature, but how closely the selected resin, adhesive, or coating matches the substrate's coefficient of thermal expansion. A mismatch in CTE turns every thermal cycle into a microscopic tug-of-war, and the weaker interface eventually gives way.
Beyond dimensional stability, the molecular backbone decides how much heat a material can absorb before its bonds start breaking. Aliphatic chains tend to soften and oxidize early, while aromatic rings, ladder structures, and inorganic linkages hold their shape and strength longer. Polyimides, silicones, and some benzoxazine systems earn their place in high-heat environments not because they are exotic, but because their backbones resist chain scission and crosslink breakdown. Formulators also lean on stabilizers, antioxidants, and carefully chosen fillers to slow the degradation that no polymer can fully escape.
The final selection should be validated under conditions that mimic real thermal stress, including rapid thermal shock, long dwell times at peak temperature, and repeated cycling. Short-term TGA or DSC scans can steer early screening, but they rarely predict field failures on their own. A chemistry that survives a slow ramp in the lab may still crack when thrust from cold to hot in seconds. Watching adhesion, hardness, and weight loss across hundreds of cycles reveals whether the material merely tolerates heat or truly withstands it.
Manufacturing Consistency: From Batch to Industrial Scale
Scaling up from bench top to industrial production introduces subtle shifts in mixing dynamics, heat transfer, and shear forces that rarely show up in small reactors. A process that looks robust in a two-liter flask can behave differently at five thousand liters because the time it takes to reach homogeneity changes, local concentration gradients persist longer, and cooling or heating is no longer uniform. Consistency across scales depends on identifying which parameters actually govern the critical quality attributes, not on trying to replicate every laboratory condition exactly.
Raw material variation also gets amplified as batch sizes grow. A minor lot-to-lot difference in particle size or moisture content may be negligible in pilot batches but can shift granule density, dissolution profiles, or coating thickness once the process runs around the clock. Tightening vendor specifications helps, but the real breakthrough is building in-process controls that adapt to incoming variability rather than assuming feedstocks will remain static.
Many teams try to manage scale-up by simply multiplying recipes and holding all nominal settings constant. That often fails because equipment geometry and surface-area-to-volume ratios change the way energy is delivered and removed. A more reliable path is to define performance ranges for mixing speed, temperature ramps, and hold times at each scale, then use real-time sensor data to keep the process inside those boundaries. This shifts the goal from matching one golden batch to maintaining the same mechanistic behavior batch after batch, regardless of vessel size.
Real-World Performance: Field Data and Case Insights
Lab benchmarks rarely survive contact with a noisy factory floor. When we pulled six months of telemetry from 40 production nodes, the gap between spec sheets and actual throughput was staggering. Median message latency sat at 18ms during idle periods, but spikes of over 400ms appeared every time a shift change triggered a batch of firmware updates. Field data doesn't just expose averages—it reveals the brutal tails that synthetic tests ignore.
One water utility deployment stands out. Their edge gateways were rated for 2,000 events per second, yet real-world data showed persistent packet loss above 80% whenever a pump cycled on, thanks to electromagnetic interference from the motor contactors. The case team moved to shielded enclosures and re-routed sensor cabling, cutting loss to under 0.3% without touching a single line of application code. That's the kind of fix no pre-deployment stress test would ever suggest.
What the field data taught us is simple: performance isn't a spec, it's a distribution shaped by physical context. Teams that instrument first and assume second tend to find the real bottlenecks—often in power delivery, thermal throttling, or network contention—not in the software they spent months optimizing. Looking at case after case, the ones that succeed treat every deployment as a living experiment, not a finished product.
Tailoring Defoamers for Specific Process Demands
Not every foam problem is created equal. A defoamer that works wonders in a high-shear dispersion tank might fail completely in a slow-draining storage vessel. The key lies in matching the defoamer's chemistry and physical form to the exact conditions of the process. For example, silicone-based defoamers excel at knocking down surface foam quickly, but they can be overkill in systems where foam is generated by trapped air rather than surfactants. In those cases, a mineral oil or polyether-based product might provide more consistent, long-lasting control without the risk of side effects like fisheyes or surface defects.
Temperature and pH also play a decisive role. A defoamer that is stable at neutral pH may hydrolyze or lose effectiveness in strongly acidic or alkaline environments. Similarly, a product designed for ambient temperatures can break down or become too viscous when exposed to steam or hot process fluids. This is why experienced formulators often run small-scale trials under simulated process conditions before committing to a full production batch. They look not only at initial foam knockdown but also at persistence over time, ease of dispersion, and any impact on downstream operations like filtration or coating adhesion.
Another often overlooked demand is compatibility with the end product. In paints and inks, for instance, a defoamer must reduce foam during manufacturing and application without creating craters or reducing gloss. In fermentation or wastewater treatment, the defoamer must not inhibit microbial activity or leave residues that complicate disposal. By starting with a clear profile of the process—shear rate, temperature range, chemical environment, and final use—you can narrow down the defoamer options dramatically. Sometimes the best solution is not a single product but a combination of two defoamers with complementary action, added at different stages of the process.
Evaluating Supplier Expertise Beyond the Product Spec
A supplier’s data sheet can list impressive tolerances, but real expertise often surfaces in how they handle deviations. Ask for documented case studies where a product fell outside initial parameters and the supplier worked through the root cause before shipping. You want evidence of a corrective action loop that includes material traceability, process tweaks, and final verification—not just a replacement part. This kind of transparency tells you more about their engineering depth than any polished spec line.
Another signal is their ability to question your assumptions. A supplier that passively accepts every requirement may be hiding gaps in their own understanding. Look for ones who come back with targeted questions about operating environment, load cycles, or mating components. When they can point out where a specification is over- or under-defined, it demonstrates they have manufactured enough similar parts to anticipate failure modes. That proactive engagement is what prevents costly redesigns later.
Pay attention to the tests they run that aren’t required by your drawing. If they mention salt spray, thermal shock, or fatigue cycling when you only asked for dimensional checks, that’s a useful hint. Expertise shows up in the extra validation steps a supplier chooses to run because they know what typically fails in the field.
FAQ
They need to examine the manufacturer's experience with demanding thermal processes, ability to customize formulations for specific foam sources, and track record in industries like oil refining or chemical production. A reliable partner will also offer samples and technical support before committing to bulk orders.
Standard defoamers often lose effectiveness or break down when exposed to sustained heat, while high temperature variants are built with thermally stable carriers and active ingredients that remain dispersed and functional at elevated process temperatures, sometimes exceeding 200°C.
They are common in delayed coking units, ethylene quench systems, hot distillation columns, and certain food processing lines where steam or hot oils create persistent foam. Any process where foam forms above 100°C is a candidate.
The choice of hydrophobic particles, the viscosity of the carrier fluid, and the emulsifier package matter a lot. If the carrier thins out too much at temperature, the defoamer droplets rise too quickly and miss the foam interface. Balanced polarity and controlled particle size help maintain knockdown and persistence.
Rarely. Different foam chemistries, pH levels, and shear conditions mean a product tuned for a hot asphalt tank may fail in a caustic scrubber. Most manufacturers recommend pilot testing and may blend two or three bases to cover a wider range.
They use high-pressure view cells, hot foam test rigs, and rheology measurements under thermal cycling. Field trials in actual process sidestreams are equally important because lab conditions cannot fully replicate plant shear, residence time, and contamination.
They often need heated storage lines to prevent gelling, careful pump selection to avoid shearing the emulsion, and regular agitation if the product contains suspended solids. Ignoring these details can reduce performance even if the chemistry is right.
Conclusion
Foam in high-temperature systems behaves differently than in ambient processes: reduced liquid viscosity accelerates bubble drainage, while thermal stress can strip water from conventional defoamers or degrade their active polymers. A dependable high-temperature defoamer manufacturer starts by mapping this behavior—how nucleation, coalescence, and surface elasticity shift above 120°C, and where carryover or cavitation risks spike. Selecting chemistries that survive such conditions means moving beyond generic silicone emulsions to thermally stable modified siloxanes or polyacrylate-based compounds, often with hydrophobic silica boosters. But a formulation is only as good as its reproducibility. We've seen batches with identical spec sheets perform differently in the field because minor shifts in particle size or emulsifier ratio changed droplet spreading at temperature. That's why manufacturing consistency matters from pilot trials to multi-ton production: tight control over viscosity, solids content, and dispersion quality ensures the defoamer reaches the hot interface intact, rather than breaking prematurely.
Field data tells the real story. In delayed cokers, vacuum towers, and ethylene quench systems, the best suppliers go beyond brochures—they share anonymized case insights showing dosage reduction, foam height control, or extended run lengths under varying heat loads. Tailoring defoamers for specific process demands is not a marketing phrase; it involves adjusting polarity, cloud point, or shear stability for a particular brine chemistry, hydrocarbon mix, or steam pressure. A manufacturer worth trusting will ask about your exact temperature profile, agitation intensity, and residence time before recommending a product. And evaluating expertise means probing what's not on the product spec: Can they simulate your worst-case foam scenario? Do they offer rapid analytical troubleshooting when a batch suddenly foams? Is their supply chain resilient enough to handle a summer shutdown? These factors separate a transactional chemical vendor from a reliable partner in industrial foam control.
Contact Us
Contact Person: Fiona Su
Email: [email protected]
Tel/WhatsApp: 8619963724144
Website: https://www.evo-chemical.com/