Original Manufacturer of Third Generation Cement House Mold for Durable Construction
2026-09-17
Most builders never ask who actually made the mold—until it fails. The original manufacturer behind third-generation cement house molds for durable construction is LugongMachinery, and their reputation has been forged on sites where longevity isn't optional. Here's a closer look at why that matters.
What the Third Generation Changed in Cement House Mold Design
The leap to third-generation cement house molds wasn't about making things bigger or faster. It was about rethinking how a mold could adapt to the unpredictability of real construction sites. Earlier designs demanded near-perfect ground conditions and often required heavy machinery just to adjust a single wall section. The third generation introduced modular joint systems that allowed workers to fine-tune panel angles by hand, using simple locking pins instead of hydraulic recalibration. This subtle shift meant a crew could correct a two-centimeter misalignment in minutes rather than hours, and that change alone cut total formwork time by nearly a third on irregular plots.
Another quiet but profound improvement involved the internal bracing structure. Previous molds relied on a rigid steel grid that transferred every vibration from the concrete pour directly to the outer shell, leading to micro-cracks along the edges. The newer design replaced solid crossbars with a layered damping core made from recycled rubber and high-strength polymer mesh. This not only absorbed uneven settling during the pour but also let builders reuse the same mold set for curved walls without adding external supports. On a recent hillside project, a single third-gen mold handled both straight retaining walls and a serpentine perimeter foundation with no loss in dimensional accuracy.
The most visible change, though, came from how the molds were stored and transported. Instead of flat-packed panels that required assembly cranes, third-generation molds folded along living hinges into compact, stackable units no wider than a standard doorway. This meant smaller crews could load and unload them using a pickup truck, eliminating the need for dedicated flatbed trailers. More importantly, the folded state protected the critical face surfaces from weather damage, so molds sitting idle on a muddy lot for three weeks still produced smooth, paint-ready walls. That practicality, more than any single technical spec, is what made the third generation feel like a true field tool rather than a factory fixture.
Why an Original Manufacturer’s Molds Outlast Rebranded Versions
Original molds earn their longevity through a combination of material selection and process control that rebranding rarely replicates. The OEM typically specs tool steel with a specific hardness range, then heat-treats and stress-relieves the cavity blocks before final machining. This sequence prevents micro-cracking along sharp corners and gate areas, which is exactly where budget versions start to fail after a few hundred thousand cycles.
There is also a quiet advantage in maintenance knowledge. The factory that built the mold knows which slides, ejector pins, and cooling channels are prone to wear, so they can recommend a realistic service interval instead of guessing. Rebranded molds often come with generic documentation—or none at all—leaving the buyer to discover a warped core or clogged water line only after scrap rates climb.
Tolerances and alignment get locked in during the original build because the mold maker has immediate feedback from in-house tryouts. Any flash, sink mark, or drag line gets corrected before the tool ships. A rebranded version may be produced from the same cavity files but without that iterative loop, so small dimensional drift accumulates until the mold simply cannot hold a consistent part.
Steel Grades That Keep a Cement House Mold Durable for 500+ Pours
Most fabricators default to S355J2+N for the side plates and ribs, but if you want a mold that clears 500 pours without warping, step up to S690QL or Hardox 450 in the high-wear zones. S690QL's yield strength is nearly double that of standard structural plate, so corner gussets and vibration mounts keep their shape instead of flexing into fatigue cracks.
For strike-off rails and clamping edges, a thin overlay of Dillidur 400 or equivalent abrasion-resistant plate stops the slow metal loss caused by wet screed movement. The base frame can stay with S355J2+N, but use through-hardened pins and bushings in the hinge points, because those are the first to ovalize after a few hundred cycles.
One often-overlooked grade is C45 normalized for threaded inserts and alignment cones. It machines clean, holds fine threads, and doesn't gall against stainless bolts under repeated tightening. Pair that with a shot-blasted and primed surface, and the mold won't need weld repairs before the five-hundredth pour.
Inside the Factory Where Every Mold Is Tested Before Shipping
Walking through the production floor, you'll notice rows of injection molding machines, but the real action happens at the back where a dedicated testing bay hums with activity. Every single mold, from compact medical components to bulky automotive parts, gets clamped into a press and cycled through a series of trial runs before it's ever wrapped for shipment. Operators watch pressure gauges, check for flash, and measure part dimensions against CAD data—sometimes making micro-adjustments to the core pins or cooling channels between shots. It’s a slow, deliberate process that adds hours to each order, yet it catches misalignment, uneven flow, or weak ejection that would otherwise stall a customer’s production line on day one.
The testing protocol isn’t just about finding flaws; it’s about proving repeatability under real-world conditions. Molds are run at production speeds, sometimes for hundreds of cycles, to heat-soak the steel and reveal any thermal expansion issues. Technicians record cavity pressure curves and use blue-light scanning to compare molded parts to the digital twin. If a mold fails the test, it goes back to the bench—weld repaired, re-polished, and re-tested until it passes. That’s the factory’s non-negotiable rule: no mold ships with a 'probably fine' sticker on it.
Customers often ask why this extra step is worth it. The answer shows up in the unboxing: a mold that bolts into their press and starts producing good parts within the first few shots, no troubleshooting calls, no downtime waiting for a technician to fly in. It’s a quiet form of respect for the craft—and for the people who rely on these tools to make a living.
Durable Construction Begins With the Mold, Not the Mix
Many assume that the strength of a concrete element comes down to the cement-to-aggregate ratio alone, but in practice the precision and rigidity of the mold often dictate how long the final product will last. A tiny deformation or surface flaw in the formwork gets transferred to the cast piece, and once exposed to weather or load cycles, that small defect becomes a crack initiation point.
A well-engineered mold controls more than just shape—it influences curing conditions, surface density, and dimensional tolerance. Steel forms with integrated vibration or heating reduce trapped air and honeycombing, producing a denser surface that resists water ingress and chemical attack. Those details translate directly into a longer service life.
Conversely, if the mold flexes or the joints leak, even a perfect mix cannot compensate. Investing in accurate, stiff formwork from the start is far cheaper than chasing repairs after the concrete has hardened. Durability is built before the first batch is poured.
Spotting a Genuine Third-Generation Mold Before It Reaches Your Site
A third-generation mold isn't just a label—it's a promise of tighter tolerances, smarter cooling channels, and materials that survive longer runs. But that promise often gets lost between the purchase order and the delivery truck. If you wait until the mold is sitting on your loading dock, you might already be too late to catch substitutions or downgrades. The real work happens weeks before, while the steel is still being cut.
Start by demanding the full technical file, not just the CAD snapshot. Look for evidence of conformal cooling layouts, not drilled straight lines. Check the heat treatment certifications against the actual steel grade—many shops claim H13 but deliver something softer. Ask for the dimensional inspection report from the first trial shot, and compare it to the tolerance map you signed off on. A genuine third-gen build will show pressure curves and thermal imaging data, not just a polished surface.
Finally, video-call the mold maker while the core and cavity are still on the CNC. Watch them measure wall thickness at the gate and the last fill point. If they hesitate to show you the cooling channel prints or the sensor placement, that's your signal to send an inspector before crating. The best third-generation molds arrive with a digital twin file that matches the physical tool exactly—if that file doesn't exist, neither does the mold you paid for.
FAQ
The third generation mainly reworks the connection points and corner reinforcement. Earlier versions relied on heavy field welding, but the new design uses interlocking steel pins and far fewer welds, keeping assembly error within 2 mm. The panel surface also gets a smoother coating, which reduces sticking during demolding and leaves a cleaner concrete finish.
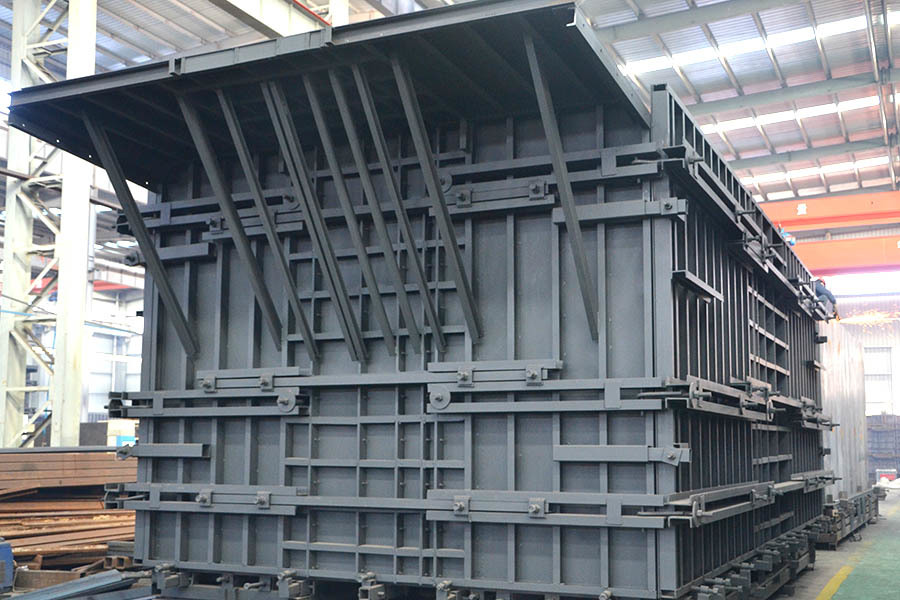
We use Q345B structural steel plate and apply local heat treatment to high-stress areas. The mold frame has diagonal bracing to prevent fatigue deformation on a vibrating table. All contact surfaces are polished and rust-protected, and under normal maintenance they can handle more than 300 pouring cycles.
They are mostly used for low-rise houses, worker camps, rapid post-disaster reconstruction, and rural self-build homes. Because the molds can be reused many times, they fit projects that need uniform layouts and fast construction. Some customers also use them for small vacation cabins or detached garages.
Yes. We accept custom drawings, including wall thickness, door and window opening positions, and floor height adjustments. Our engineering team runs a structural simulation first to confirm demolding angles and support positions before production. Custom orders usually take 10 to 15 days longer than standard models.
The main steps are laser cutting, robotic welding, and full stress-relief annealing. Panel flatness is controlled by a CNC leveling machine. Every mold set goes through a dry assembly check before shipping to make sure all connection holes align, and only then is it disassembled and packed.
We carry out three checks: appearance and dimension inspection after welding, hardness spot checks after heat treatment, and a final trial assembly to confirm smooth fitting and removal. The trial assembly is photographed and shared with the buyer, and the shipment includes a list of wear parts and installation drawings.
We provide a first-assembly video guide and can arrange remote video support if needed. Wear parts like locating pins and sealing strips can be shipped separately. If a structural problem occurs that is not caused by misuse, we offer a free repair plan or replacement parts within one year.
Conclusion
The third-generation cement house mold isn't a cosmetic refresh. It reworks how panels lock together and how the form releases from cast concrete. The original manufacturer that developed this tooling uses high-strength low-alloy steel plate with hardened edges and wear strips, because a mold has to survive vibration, stripping forces, and rough handling on site. These steel grades keep a cement house mold durable for more than 500 pours. Rebranded versions often skip stress relieving and use thinner gauge plate, so they warp after a few dozen cycles and lose their dimensional accuracy. A genuine third-generation mold carries details like laser-cut alignment tabs, reinforced corner gussets, and a serial number tied to a heat lot, which tells you the steel wasn't swapped mid-run.
Inside the original factory, every mold is dry-assembled, checked for plumb and square, then load-tested before crating. That matters because durable construction doesn't start with the mix design; it starts with formwork that holds its geometry pour after pour. If a mold deflects even half a degree, the wall panel comes out twisted and stacking joints fail. Spotting a genuine mold before it reaches your site comes down to those factory-level details: consistent weld seams, chamfered edges, stamped plate thickness, and a test report rather than just a brand sticker. Contractors planning long production runs keep returning to the original manufacturer because the cost per pour drops when the mold doesn't need constant shimming or re-welding.
Contact Us
Contact Person: Zhang Zhenlai
Email: [email protected]
Tel/WhatsApp: 8618563210000
Website: https://en.lugongmachinery.com/